
Switching baking trays is a production decision before it is a packaging decision. A tray that looks right on a sample table can still slow a depositor, misbehave in a tunnel oven or crush on a pallet. A structured line trial answers those questions with your own product, on your own equipment, before any volume is committed.
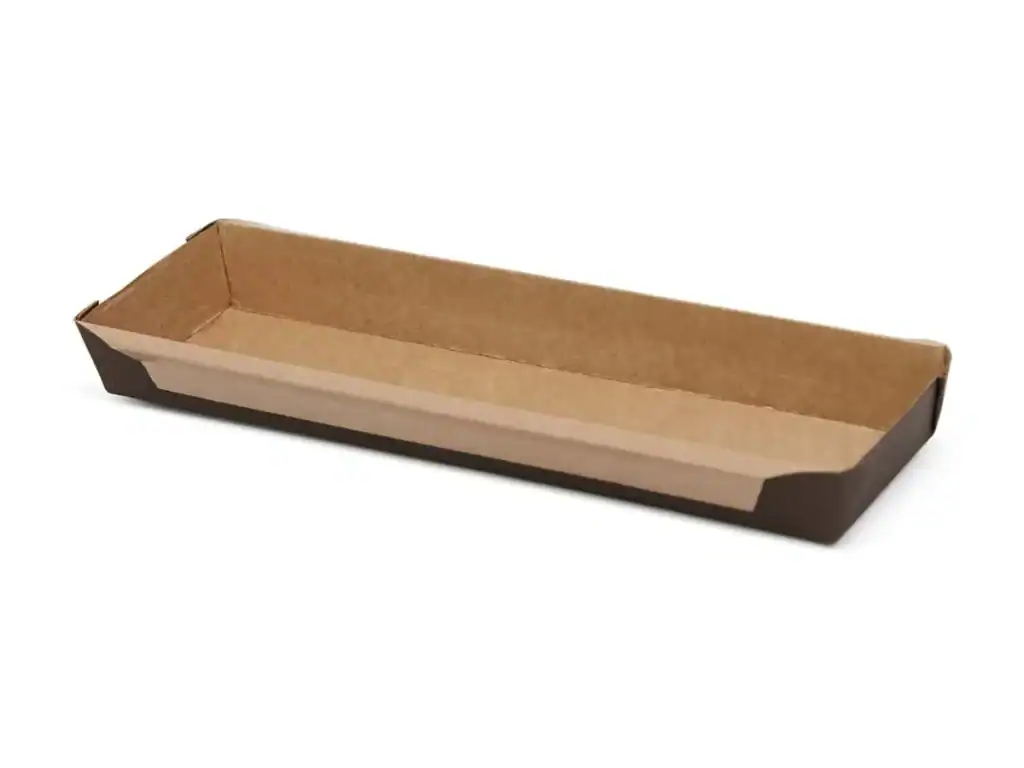
This guide sets out the protocol we use when a bakery or food manufacturer trials G-Flute trays against the tray it uses today.
1. Define what the trial must prove
Agree the decision criteria before the first tray is filled. Most trials come down to four questions:
- Does it run? The tray feeds, de-nests, fills and travels through every station without stoppages.
- Does it bake? The product reaches the same colour, volume and core temperature as in the current tray, within the same oven profile.
- Does it hold? The tray keeps its shape through cooling, freezing, packing and transport, with no leakage or release failures.
- Does it pay? The total cost per finished unit is lower, or the same with a clear commercial benefit.
2. Prepare the baseline
A trial is only as good as the comparison. Record the current situation over at least one full shift:
- Line speed and stoppages per hour, by cause
- Oven profile: temperatures by zone, belt speed and bake time
- Reject rate at each inspection point
- Labour steps around the tray: de-panning, greasing, washing, re-stacking
- Landed tray price per unit, including freight and storage
3. Match the format to the line
Share drawings or measurements of the current tray, the depositor pitch and the conveyor widths. The closest standard format is selected first; if none fits, a custom size is proposed. Board grade and finish are chosen by product: wet batters and fatty fillings usually call for a barrier finish, dry doughs often run on kraft.
4. Run the trial in stages
- Dry run. Empty trays through feeding, filling stations and conveyors to confirm mechanical fit.
- Short bake. A small batch through the oven at the standard profile, checked for colour, volume, core temperature and release.
- Production run. At least one full shift at normal speed, packed and stored as standard.
- Downstream check. Frozen storage, transport and, where relevant, reheating, as the product will actually be handled.
5. Measure the same things the same way
Use the baseline sheet as the trial sheet. For each metric, record the result per finished unit so the two trays can be compared directly. Photograph trays after baking and after transport, and keep samples for reference.
6. Read the result as a cost per baked unit
Tray price is only one line in the calculation. Removing de-panning, washing or greasing steps, reducing rejects and simplifying packing can outweigh a difference in unit price. The decision figure is the saving, or cost, per baked unit. Our article on total cost per baked unit explains how to build that figure.
Checklist
- Decision criteria agreed in writing
- Baseline recorded over a full shift
- Format and finish matched to product and line
- Dry run, short bake, production run, downstream check
- Results recorded per finished unit
Planning a trial? Tell us about your line and we will propose a format and send samples.